Fully Automatic Rotary Concrete Reclaimer for Export: Smart Solutions for Efficient Concrete Recovery
2026-08-31
Most ready-mix plants lose money in the sludge they wash away. A fully automatic rotary concrete reclaimer changes that equation—recovering aggregates, recycling water, and running with minimal supervision. In this article, we look at how Sinou designs these systems for international buyers who need efficiency without complexity.
Why a Rotating Drum Beats Static Settling
Static settling looks fine on paper—heavier particles drift to the bottom and clear liquid rises. But in practice, the bed that forms at the base quickly becomes a dense, sticky layer that traps water and slows everything down. A rotating drum keeps the solids tumbling, so they never get a chance to lock into that impermeable mat. The constant motion opens tiny channels through the sludge, letting trapped liquid escape far faster.
There’s also the matter of throughput. In a static tank, you're always waiting for the slowest particle to make its way down, and any disturbance stirs things up again. A drum’s rotation sets a gentle, controlled shear that brings fresh solids into contact with the screen or drainage zone over and over. It’s not just settling—it’s a continuous reset, so performance stays steady instead of fading as the sludge compacts.
Zero Attendance from Washout to Stackout
You book the room, set up the chairs, and print name tags, only to watch the door stay closed for an hour. That kind of washout can feel like a verdict, but it is more often a signal that the usual invite-and-hope approach has stopped working.
Turning that around starts with a handful of direct conversations. Ask five or ten people what would make an event actually worth their time, then shape the whole session around those answers. Swap generic promises for a concrete outcome, such as leaving with a ready-to-send outreach message instead of a vague networking hour.
Once the first few yeses are in, let them work for you. Name who is already coming, share a rough outline of what is being built, and make it easy for others to picture themselves in the room. A stackout does not need a big budget; it needs a reason that spreads person to person.
Export Friendly Design for Coastal and Inland Plants
Shipping plants across borders rarely fails because of the plant itself—it fails in the transition between humidity, salt air, and root disturbance. A practical export design for coastal and inland species starts by matching container shape to the stress profile of each group. Coastal plants with shallow, spreading roots do better in low, wide pots that stabilize against wind and reduce tipping during transit; inland species with deeper taproots need tapered sleeves that keep the root column intact without adding excess soil weight.
The real leverage comes from treating roots and foliage as one system. A lightweight, quick-draining substrate blend with coconut coir and perlite holds enough moisture for inland varieties while preventing salt buildup around coastal root zones. Pair that with a vented, wax-lined carton that maintains stable humidity without trapping ethylene, and the same crate can carry both types of plants through inspection without extra handling. The goal is not just survival on arrival but a plant that resumes growth within days, not weeks.
One Machine for Aggregate, Water, and Cement Recovery
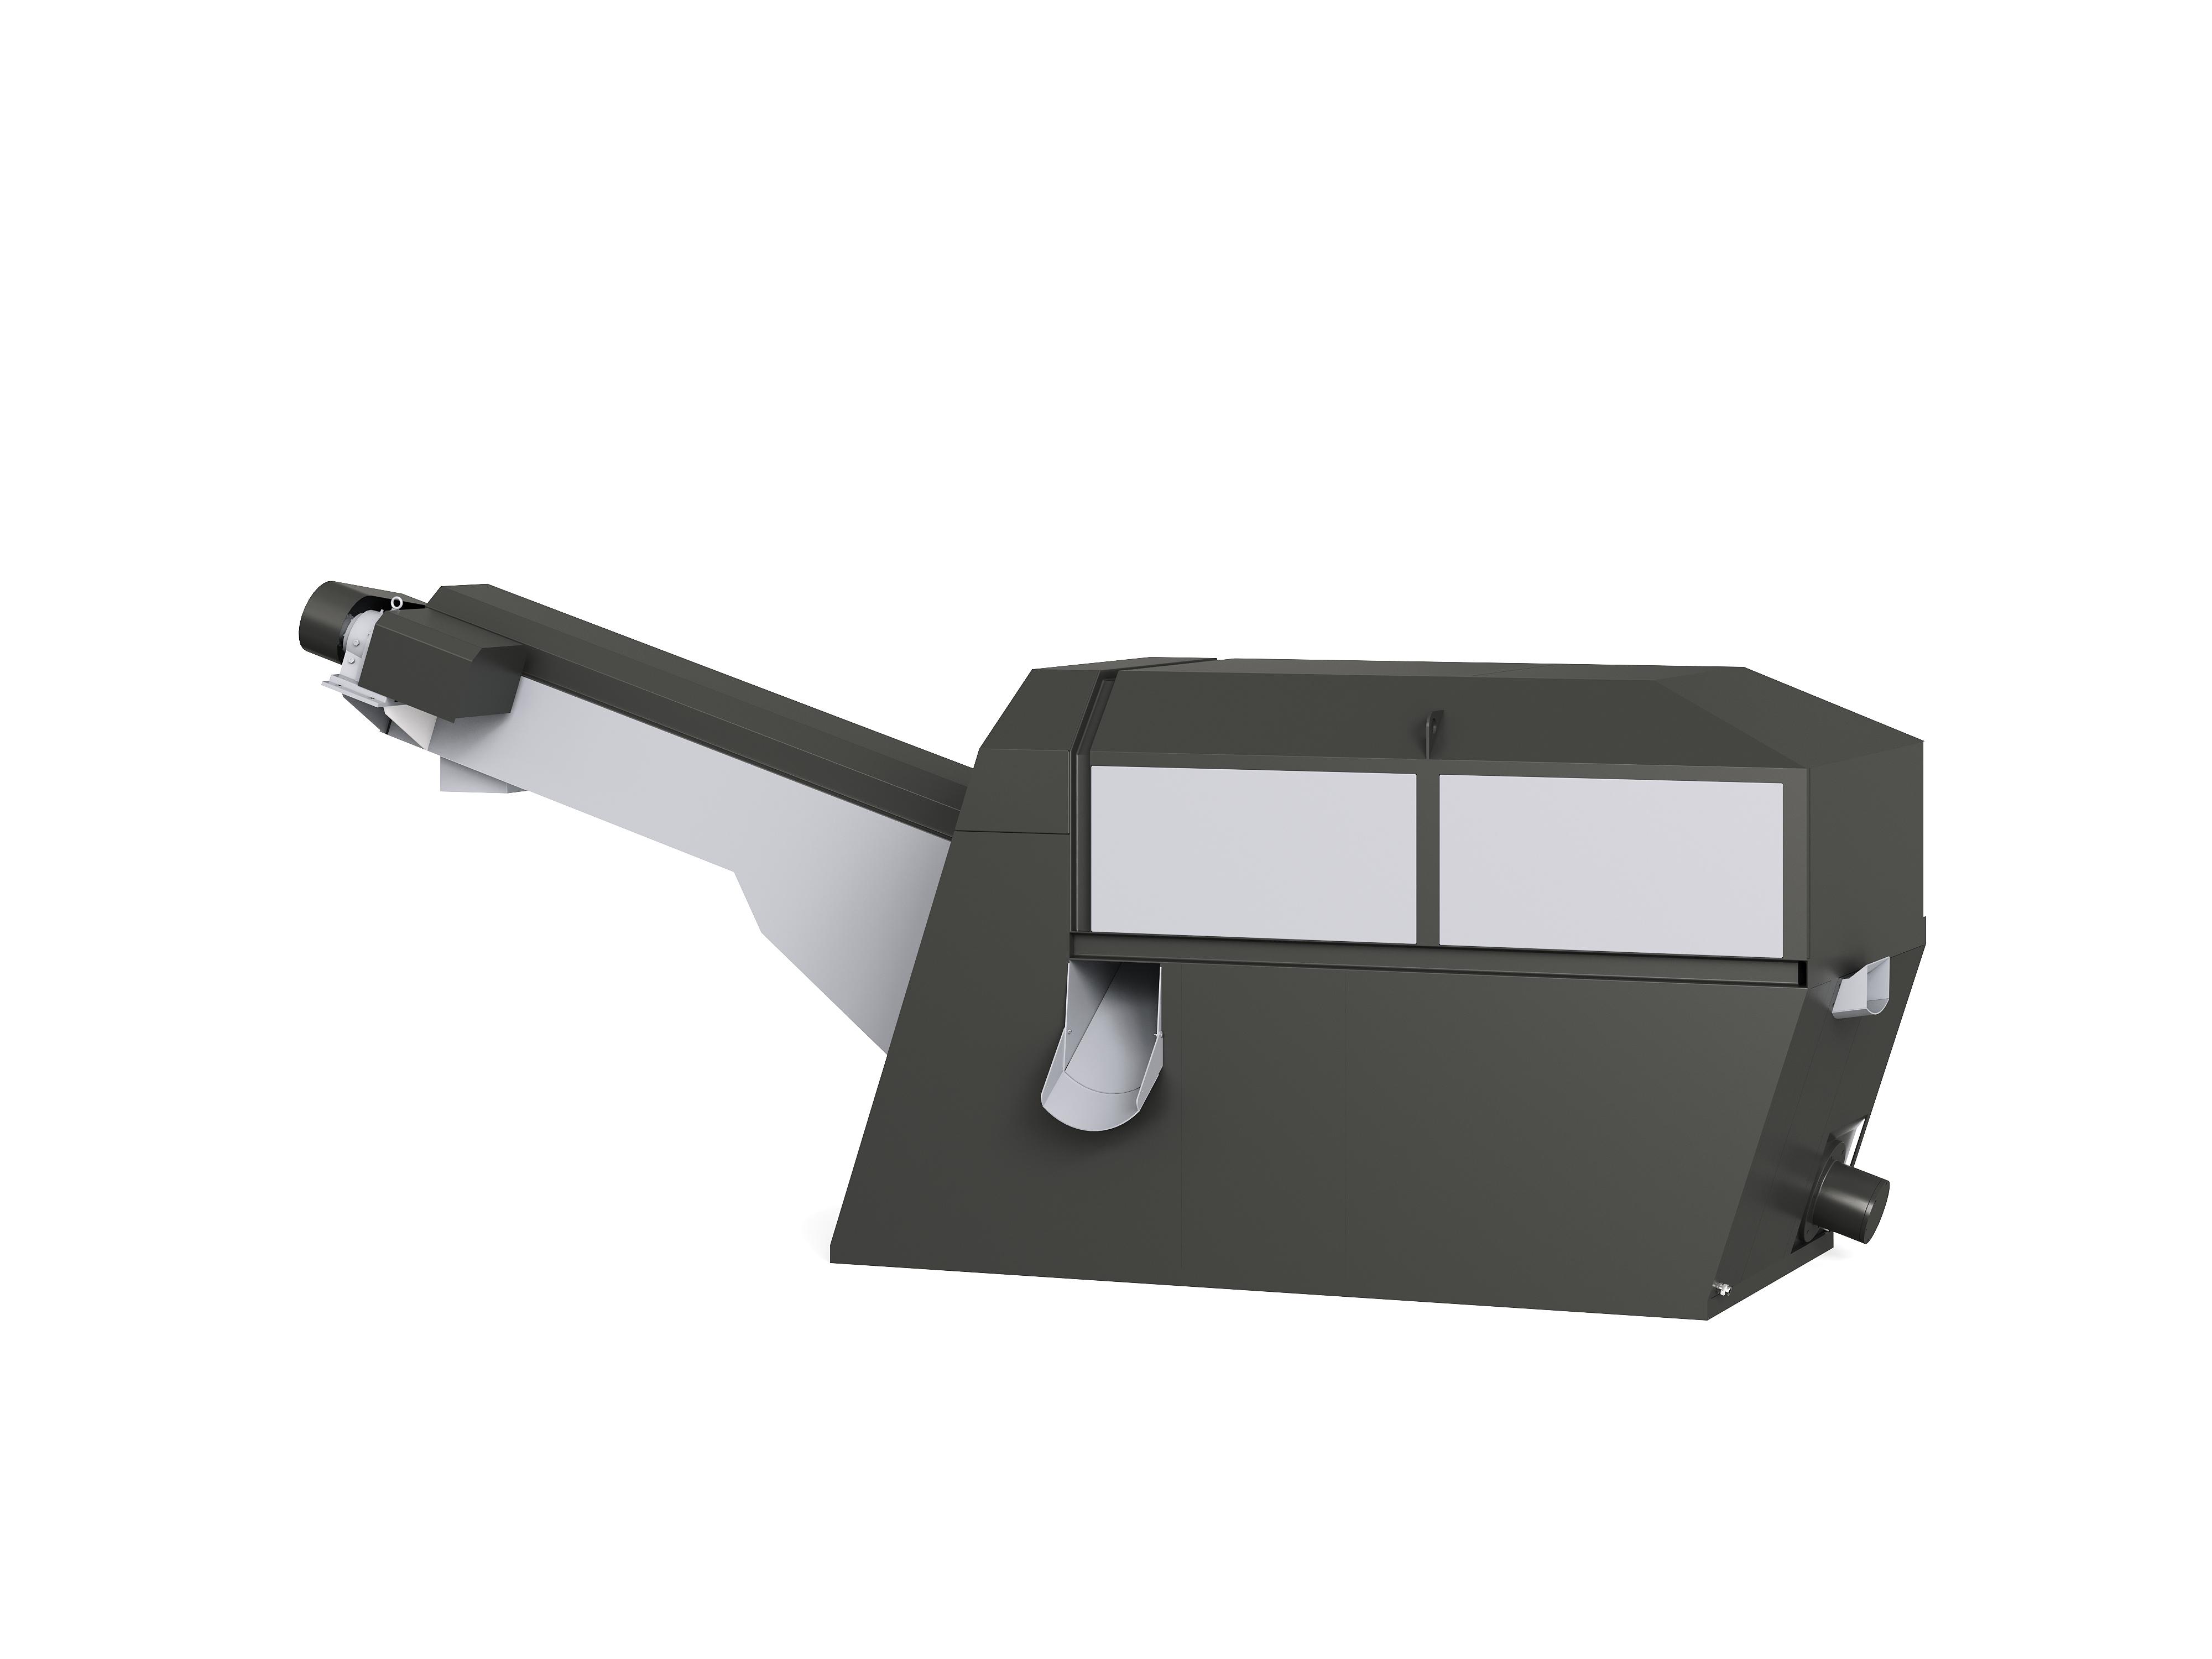
In most concrete reclamation setups, you need separate stations for screening aggregate, settling out cement fines, and reclaiming process water. This machine collapses those steps into a single continuous loop. Fresh slurry from truck washout or mixer rinsing goes in one end, and graded sand and stone come out dry enough to reuse immediately, while the water is clarified and sent back to the batching plant. The cement paste that gets washed off the aggregate is not discarded; it is collected in a fine-particle filter press or thickener that returns it as a reusable slurry for low-strength mixes or as a soil amendment base.
The trick lies in how the drum and spray bar work together. Instead of a high-speed centrifuge that shears the aggregate, a low-RPM rotating screen lifts and tumbles the material under a curtain of recycled water. That gentle action strips off the cement film without breaking down the rock. The water drains through the screen into a settling cone where the heavier fines drop out, and a series of weirs skim off the top layer of clean water. There is no need for a separate clarifier tank because the cone's laminar flow design creates a natural density gradient, so the cleanest water rises to the overflow while the sludge stays at the bottom for periodic removal.
Operators appreciate the reduced footprint more than anything else. A typical setup with a separate aggregate screener, a washout pit, and a filter press might take up half a yard and require three different pumps. This unit fits in a corner next to the wash rack and runs off a single power drop. The maintenance routine is simple: one grease fitting on the main bearing, a screen mesh that can be swapped in under twenty minutes, and a sludge valve that opens by hand. Because the water never leaves the closed loop, there is no standing pond to attract mosquitoes or freeze over in winter. When the cement content in the returned slurry gets too high for batching, the operator just drains the cone into a roll-off bin and lets it set into a low-grade fill material.
Smarter Sequencing That Matches Plant Throughput
A line that mixes standard and custom units can stall when the job order ignores changeover time between families. Matching the sequence to actual plant throughput means looking at how many units each station can absorb per hour, then spacing those family switches so setup doesn’t repeatedly eat into run time. The payoff shows up as fewer piles at the slowest machine and fewer idle minutes at the fastest.
This kind of sequencing isn’t set once at the start of the week. After each shift, the system compares planned output against what the floor really produced and adjusts the next block of work. If a downstream process falls behind, upstream jobs that don’t feed it move ahead instead. That keeps hands and machines occupied without building excess work-in-progress, and over several days the line settles into a pace that reflects its true capacity rather than an optimistic target.
Where Fully Automatic Reclaimers Pay Off Fastest
Fully automatic reclaimers deliver their strongest returns in high-volume yards where material streams rarely change. When incoming scrap is consistent—such as dedicated processing lines for demolition debris or single-grade mill scrap—the machine can lock into a steady rhythm without operator intervention. The payback comes from eliminating idle time between batches and reducing the labor needed to manage frequent choke points. In these settings, the reclaimer’s self-adjusting feed and discharge cycles keep throughput near theoretical maximum for hours at a time, turning what would be a labor-intensive bottleneck into a nearly unattended operation.
Another fast-payback environment is a facility running multiple shifts with tight labor availability. Skilled operators are hard to hire and retain, and even a modestly automated reclaimer can free up one or two people per shift for higher-value tasks like quality sampling or equipment inspection. The cost logic is simple: if a single operator spends 60% of their time babysitting a feeder and clearing jams, the automation pays for itself in under two years in most regions. This is especially true in ports or transfer stations where material arrives in unpredictable surges, but the reclaimer can buffer and meter flow more evenly than a human reacting to every spike.
Finally, fully automatic reclaimers prove their worth in enclosed or hazardous processing areas. Dust, noise, and moving machinery make manual oversight both risky and expensive in terms of PPE, monitoring, and compliance. By letting the reclaimer manage its own feed rate and clear minor obstructions automatically, facilities reduce worker exposure and lower incident-related downtime. The fastest payback often occurs in metal shredding operations or C&D recycling lines where safety regulations already demand frequent pauses for manual checks—an automated unit simply keeps working safely through conditions that would otherwise trigger a stop.
FAQ
It handles feeding, washing, separating, and discharging without manual intervention. Sensors and a programmable control panel regulate drum speed, water flow, and discharge timing so operators only need to set the batch parameters.
The inclined rotating drum creates a continuous tumbling action that breaks down wet concrete and scrubs aggregate surfaces more thoroughly than stationary tanks. This helps recover cleaner sand and stone while sending only fine cement slurry to the settling area.
Yes, it can be configured for common voltage and frequency combinations such as 380V/50Hz, 415V/50Hz, or 460V/60Hz. The control cabinet includes phase protection and is built to handle voltage fluctuations often found at ready-mix plants overseas.
Most installations recover over 95% of reusable aggregate and return about 80–90% of process water to the batching system. The exact figure depends on mix design, silt content, and how often the settling tank is cleaned.
Yes, it accepts both whole returned loads and washout from truck chutes and mixer drums. The infeed hopper is sized to take a full discharge without spillage, and the drum speed adjusts automatically for thick or slurry-heavy material.
Daily checks focus on the spray nozzles, drum flights, and discharge chute for buildup. Bearings and drive chains need lubrication every 40–60 operating hours. The wear-resistant drum liner should be inspected monthly, and replacement is usually needed only after 3–5 years in normal use.
It stores multiple mix profiles and can start or stop based on a schedule or a signal from the truck wash station. Because the sequence runs without an operator, one worker can manage several reclaimers or handle other yard tasks during the recovery cycle.
A level concrete pad with a drainage channel, a clean water supply of at least 2 bar pressure, and a settling pit or filter press connection are the main site preparations. The supplier provides anchor bolt drawings and a piping layout so local contractors can finish civil work before the unit arrives.
Conclusion
A rotary concrete reclaimer built for export has to earn its place on site, and the rotating drum does exactly that. Instead of waiting for solids to settle out of wash water, the drum keeps material moving, scouring aggregate clean and sending fines into a separate stream. That means a plant can go from truck washout to stacked aggregate without anyone standing by to nudge the process. Coastal and inland facilities alike deal with humidity, salt air, or tight space, so the frame, drives, and control cabinet are sealed and sized for container shipping—no special rigging, no on-site fabrication. The real payoff shows up in the sequencing: the machine reads the pace of returning mixers and adjusts its cycle instead of running blind. That keeps water and cement fines in circulation, cutting fresh water demand and disposal costs in one move.
The fastest return on a fully automatic reclaimer comes where truck traffic is heavy and washout is constant—think multi-plant operations or large ready-mix yards near ports. By recovering aggregate, process water, and cement slurry in one pass, a single machine replaces the old chain of settling pits, clarifiers, and front-end loaders. Operators get cleaner aggregate back into stockpiles, water that is ready for the next batch, and a slurry stream that can be dosed back into low-strength mixes. Where that matters most is in plants that already run tight margins on water and disposal. Because the machine runs unattended from washout to stackout, labor shifts to batching and delivery, not shoveling out pits. For an export-focused plant, that combination of lower operating cost, smaller footprint, and simpler site preparation makes the reclaimer a practical upgrade rather than a luxury add-on.
Contact Us
Contact Person: HaiYan
Email: [email protected]
Tel/WhatsApp: +86 18957325588
Website: https://www.senyoubeton.com/