Gold Plating Production Line Company Traits That Drive Quality
2026-08-31
Ask any plating engineer what ruins a gold line and you’ll hear the same list: inconsistent thickness, poor adhesion, bath contamination. The root cause usually isn’t the equipment—it’s the company running it. Certain traits predict quality before a single part hits the tank. Junda is built around those traits, and this post unpacks what they are.
Micron-Level Precision Without Compromise
Precision at the micron level is not just a specification—it is the quiet engine behind every reliable measurement, every seamless fit, every flawless surface. When tolerances shrink to the scale of a few microns, the margin for error disappears, and with it, any room for compromise. This is the realm where ambient temperature fluctuations, sub-micron vibrations, and even the pressure of a measuring probe can distort results. Achieving accuracy here demands more than a steady hand; it requires a system designed from the ground up to isolate, stabilize, and verify every variable that matters.
The pursuit of micron-level precision often forces a trade-off: speed against accuracy, ruggedness against sensitivity, or affordability against performance. But true engineering excellence refuses that binary. Instead, it integrates advanced thermal compensation, active damping, and real-time feedback loops so tightly that precision becomes inherent—not conditional. The result is a machine or instrument that holds its tolerance on the factory floor, in the lab, and across thousands of cycles, without constant recalibration or environmental pampering.
What sets apart a genuinely uncompromising system is its ability to prove itself, repeatably. Every axis movement, every optical reading, every machined edge carries a traceable pedigree back to national standards. And because the design anticipates error before it occurs, users spend less time chasing drift and more time trusting the output. That is what micron-level precision without compromise looks like: not a boast, but a working reality built into the bones of the device.
Zero-Defect Mindset in Every Batch
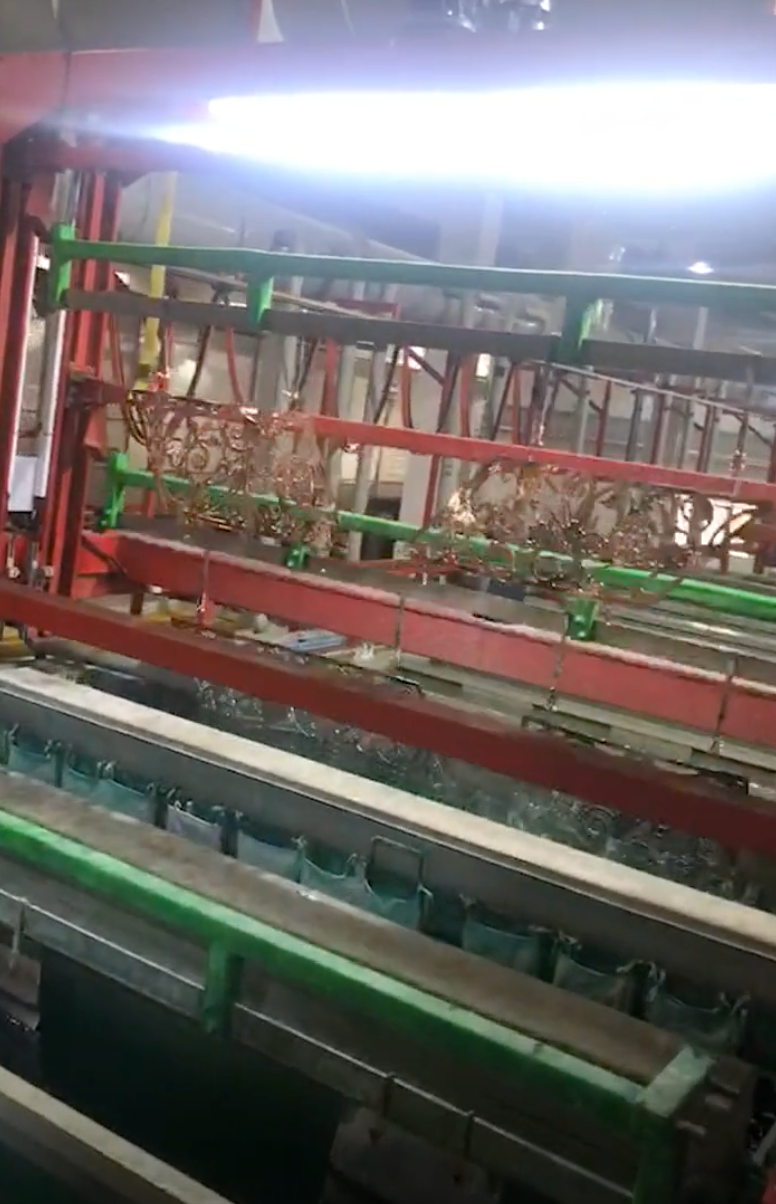
Quality is not a checkpoint we visit at the end of production. It lives inside the rhythm of every single batch. The zero-defect mindset means each operator, mixer, and packager carries the same quiet question: would I put my own name on this? That personal ownership transforms routine into a standard that cannot be faked.
We measure defects not as a percentage of output, but as a reflection of decision quality. When a batch fails, the root cause is rarely the raw material. More often it is a small assumption left unchecked, a tolerance stretched just once, a handover that skipped a detail. Zero defects does not mean perfection by luck. It means we design the process so mistakes have nowhere to hide.
Every batch becomes a promise repeated. The ingredients may change, the shift may end, but the bar does not move. New team members are taught that stopping the line to verify is not a delay; it is the job itself. This is how zero defects stops being a slogan and becomes the only way work feels normal.
Material Purity as a Non-Negotiable
Impurities aren’t just imperfections—they’re failure points waiting to surface under load, heat, or time. A few parts per million of the wrong element can shift conductivity, weaken a weld, or cause premature corrosion. That’s why purity isn’t treated as a target to aim for, but as a hard line that doesn’t move.
Every incoming batch gets tested against a strict specification, not a vendor’s word. Certificates of analysis are checked, but we don’t stop there—independent sampling and verification happen before anything enters production. Materials that fall short, even by a fraction, are rejected outright. No blending, no “close enough,” no rework to mask the problem.
This stance costs more at the front end, and it slows things down. But it eliminates the hidden costs that come later: field failures, recalls, and eroded trust. When purity is non-negotiable, every downstream decision gets simpler.
Live Process Feedback, Not Just Periodic Checks
Most teams still rely on quarterly reviews or monthly reports to gauge how a project is going. That approach leaves huge gaps between observation and action. By the time a manager notices a recurring bottleneck, weeks of compounding delays have already set in. Live process feedback closes that gap by surfacing issues as they happen, not after the fact. It turns process improvement from a scheduled event into an ongoing conversation.
Making feedback immediate doesn't require sophisticated tooling. Simple mechanisms like a shared dashboard showing cycle times, or a lightweight bot that pings a channel when a work item sits idle beyond a threshold, can be enough. The key is to treat feedback as a stream rather than a snapshot. Teams that adopt this mindset stop defending their current workflow and start refining it continuously. They notice small friction points early and adjust before they harden into habits.
There's also a human side to this. When people see the direct consequences of their actions in near real time, they feel more ownership over the process itself. Waiting for a formal review can make improvement feel like an external demand. Live feedback makes it a shared, self-correcting rhythm. That shift often does more for team morale and output quality than any periodic check ever could.
Operator Expertise Backed by Data
On the factory floor, intuition still carries weight. But the operators we trust most are the ones who pair hard-won instinct with a steady feed of real numbers. They know the hum of a healthy machine, yet they also pull up shift logs, vibration readings, and output variance before making a call. That blend of gut and data turns a good operator into a reliable decision-maker under pressure.
What separates a reactive fix from a proactive save is often the quiet work done between alarms. Skilled operators don't just react to what the dashboard flashes; they cross-reference historical patterns, maintenance records, and even subtle trends in material quality. A sudden temperature spike might mean nothing by itself, but combined with a slight drop in throughput and last week's bearing replacement, it tells a story. Data doesn't replace expertise, it sharpens it.
Training programs are catching on. Instead of handing over a manual and a pat on the back, smart facilities embed data literacy into operator development. New hires learn to read the same charts they'll rely on at 3 a.m. when things go sideways. The result isn't a desk-bound analyst pretending to run a line; it's a hands-on expert who can argue with a spreadsheet and win. And when that operator says something feels off, people listen—because the numbers usually back them up.
Continuous Tuning for Consistent Shine
A flawless reflection doesn't come from a single pass. It's the result of reading the surface as you work—feeling how the pad responds, watching how the product breaks down, and adjusting speed, pressure, and arm movement on the fly. This kind of continuous tuning turns an ordinary polish job into a deep, liquid shine that looks the same from every angle.
Every panel has its own quirks. Curves, edges, and paint hardness shift from one section to the next, and even the room temperature can change how a compound behaves. By staying attentive and making small, real-time corrections, you avoid the flat spots and haze that come from a rigid, one-setting approach. The result is a more even finish without chasing defects later.
Consistency isn't about repeating the exact same motion every time—it's about adapting so the outcome stays identical. That means checking your work under different light sources, revisiting areas that look slightly dull, and trusting your hands over any preset dial. When you tune continuously, the shine doesn't just peak once; it holds steady across the whole surface.
FAQ
The ones worth keeping don't lean on a single shiny certification. They run small-batch validation before full production, keep a repair log that shows recurring weak points, and their engineers will tell you the limits of their own rectifiers rather than promising impossible tolerances.
Far more than most buyers assume. A well-baffled tank with deliberate anode placement lets you hold thickness within a few percent on corners and recesses. Poorly placed anodes will force you to overplate flat areas just to meet minimums in tight spots, which wastes gold and creates dimensional issues.
Chemistry is only half the story. Adhesion usually fails because the activation and rinse sequence before plating was rushed, or because the base metal had invisible smut from polishing that no cleaner removed. A quality-driven line documents surface prep times and checks rinse water quality daily instead of assuming the chemistry will fix everything.
A rectifier that drifts by even a few percent can shift deposition rates enough to push a borderline part out of spec. Companies that care about quality pull rectifiers for calibration on a fixed schedule and log the ripple readings. Without that habit, two lines running the same recipe can produce noticeably different results.
Absolutely. Racks that allow parts to touch or shield each other create uneven current density and rub marks. Better companies use custom fixtures that hold parts at controlled angles and have dedicated storage so finished pieces aren't stacked against raw ones, reducing post-plating handling damage.
Look for work instructions that name specific temperatures, currents, and dwell times rather than vague ranges. Also check whether the documentation includes a defined out-of-spec response, like quarantine and root cause. If the manual reads like a sales brochure, the production floor probably doesn't use it.
They can walk backward from the part serial number to the exact tank, rack, operator, and rectifier settings used that shift. They keep bath analysis logs and maintenance records tied to the same timeline. That lets them spot whether the failure came from a chemical imbalance, a training gap, or a hardware drift instead of guessing.
There is, though it shows up in subtle ways. Operators trained in troubleshooting can catch a dropping bath temperature or a clouding rinse before it ruins a rack. Companies with shallow training rely on inspectors to catch defects after the fact, which drives rework rates up even when the line equipment is identical.
Conclusion
What separates a high-performing gold plating line from an average one is rarely the equipment catalog—it's the refusal to accept "close enough." Every deposit is measured at the micron level, with thickness tolerances treated as hard limits rather than suggestions. A deviation that would pass elsewhere triggers immediate rework, because the team understands that a few microns of variance can change corrosion resistance and electrical performance. That zero-defect discipline carries into every batch; jobs are not processed as bulk goods but as individually accountable runs, each with its own traceable history. Material purity sits on the same non-negotiable ground. Gold salts, brighteners, and rinse water are vetted at the source, and impurities are kept out of the tanks. Once contamination enters the bath, it shows up on the final surface—so the only way to guarantee a clean finish is to never let it in.
Periodic sampling alone cannot protect a plating line from drift. Sensors and inline analyzers track current density, temperature, pH, and agitation in real time, feeding live data to the operators instead of waiting for end-of-shift reports. That feedback loop is what turns an experienced technician into a precise decision-maker. When a parameter shifts by a fraction, the team adjusts on the spot—not after a defect has already been plated. This constant tuning is aimed at one thing: repeatable brilliance. By logging every variable for every run, the company builds a living record that turns past batches into smarter future ones. The result is not occasional shine, but the same mirror-like, uniform finish on the first part of the day and the last.
Contact Us
Contact Person: hayyr
Email: [email protected]
Tel/WhatsApp: 8613082110525
Website: https://www.jundaelectroplating.com