Plastic Sheet Machine Company: Key Factors for Choosing the Right Manufacturing Partner
2026-10-16
Choosing a plastic sheet machine company often feels like reading a spec sheet—everything looks identical until production starts. The real decision isn't about horsepower or screw diameter alone; it's about the manufacturing partner's ability to solve problems before they reach your floor. If you're tired of vendors who disappear after installation, the conversation changes. COMRISE approaches each line as a long-term engineering commitment, not a one-time sale. Below, we break down the factors that actually matter when evaluating a partner, so your next purchase doesn't become an expensive experiment.
Can They Run Your Material Before You Sign?
Ask whether they can run your exact material before you sign—not just a close cousin from the same family. A shop might say they’ve machined plenty of aluminum, but your 7075-T6 with a tight anodize spec behaves differently than 6061. Request a trial run on your supplied stock, even if it’s a small batch. Watch how they handle warping, burrs, or tool wear. If they push back or say ‘we’ve done similar,’ that’s worth a second thought.
Running your material is also a test of their communication. Do they send photos mid-run, flag a surface finish issue, or just hand back parts and hope you don’t notice? A vendor who documents setup changes and calls you about a shrink rate variance is one you can trust later. The trial isn’t just about machine capability—it’s about whether they treat your material as a puzzle to solve or a job to push through.
Finally, clarify the cost before anything hits the spindle. Some shops do a free sample run if you cover shipping, others charge a setup fee that gets credited once you place a production order. A clear answer here tells you how they handle small commitments. If the trial run terms are vague or loaded with fine print, assume the production contract will be too.
What Does Their After-Sales Support Actually Look Like?
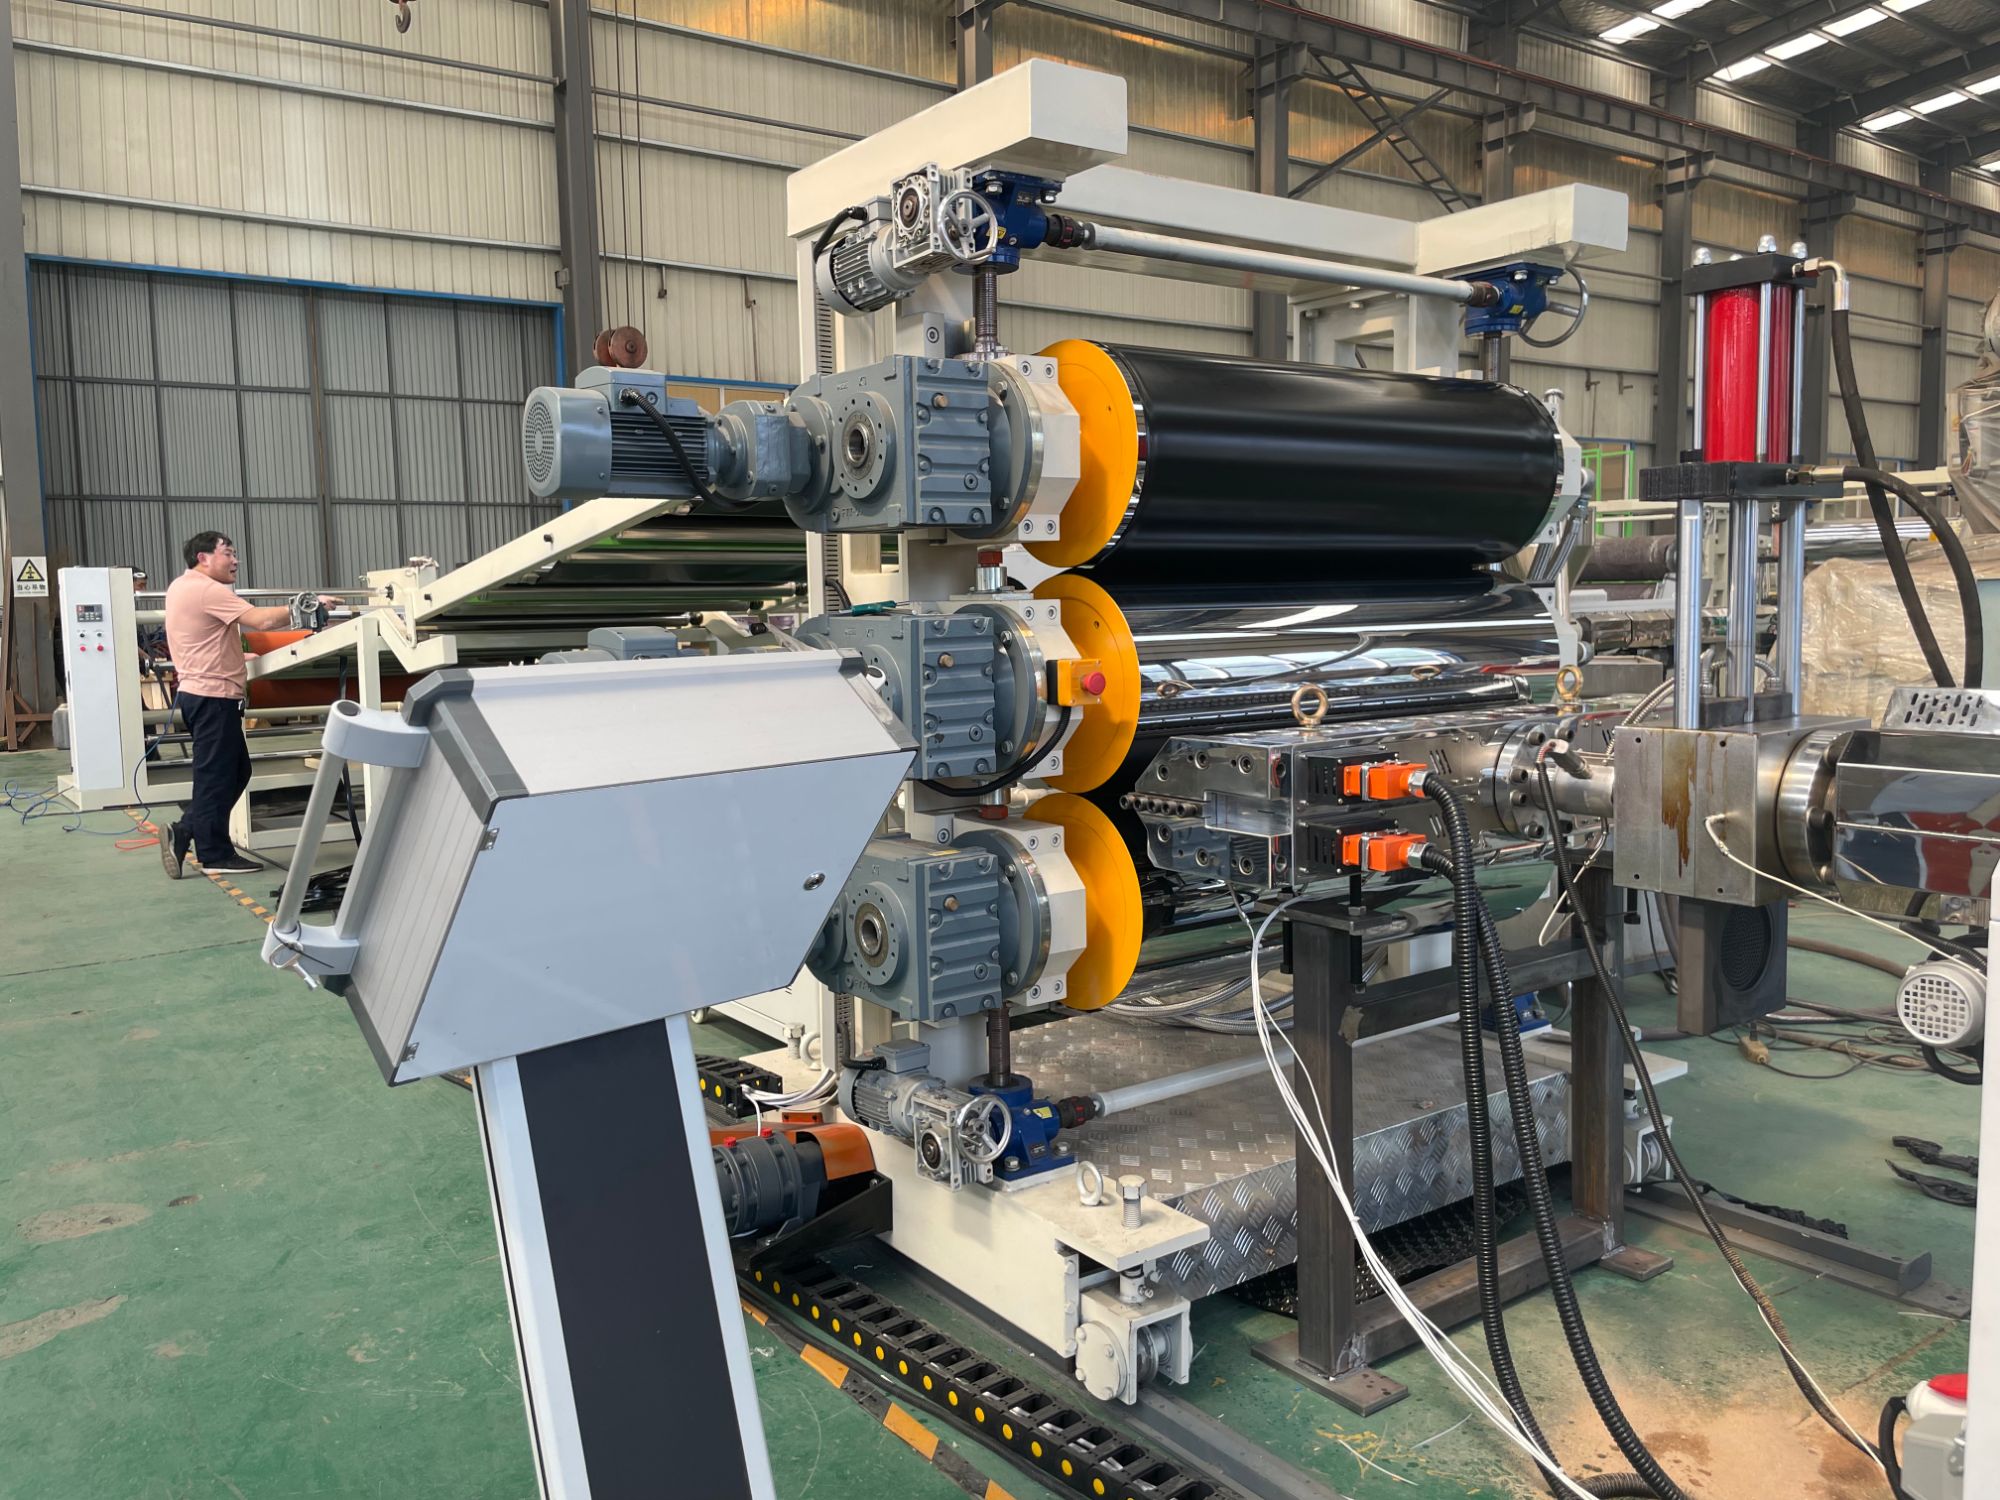
After unboxing their product, you might assume the relationship ends once the payment clears. But a closer look at their post-purchase workflow reveals a team that treats support as an ongoing conversation rather than a one-off transaction. Their reps don’t just shuffle you through a scripted checklist. Instead, they ask about your specific setup, note the quirks of your usage, and offer tweaks that actually fit your day-to-day routine. It’s the kind of follow-up that feels less like a help desk and more like a neighbor who happens to know the product inside out.
What stands out most is how they handle the messy, unglamorous issues. A broken latch on month eleven? They’ll ship a replacement part without demanding a five-minute video proving you didn’t drop it. A software glitch that only appears when two features overlap? Their engineers reproduce the bug themselves, then email you a patch before you’ve finished your morning coffee. No canned apologies, no “we value your feedback” filler. Just a clear timeline and a person who actually owns the problem until it’s fixed.
The hidden gem is their proactive outreach. About two weeks after delivery, you’ll get a plain-text email asking how the product is settling in — not a survey link, but a real question from a named support agent. Reply with a gripe, and they’ll follow up with a phone call. Stay silent, and they won’t pester you. That restraint is rare. It signals they trust the product to do its job, and when it doesn’t, they’re already reaching for the toolbox instead of the script.
How Much of the Machine Is Built In-House?
Most companies keep this number vague, but the reality here is that nearly 70% of the core mechanical and electrical systems are designed, machined, and assembled on our own floor. That includes the drivetrain, control boards, and the firmware that runs them. The remaining 30%—things like power supplies, display panels, and certain bearing sets—comes from specialized suppliers, mostly because it would be impractical to reinvent components that are already produced at higher precision and lower cost elsewhere.
There’s a practical reason for drawing that line where we do. In-house work gives us direct control over tolerances and revision cycles. When a customer reports a fault, our engineers can walk to the prototyping area and test a new bracket or a revised control loop the same afternoon. Outsourced parts don’t offer that kind of responsiveness, so we only rely on them when the supplier’s expertise clearly outweighs the benefit of keeping it internal.
Of course, “built in-house” can be a marketing phrase more than an engineering fact. We tend to avoid that game. The more useful question is whether the parts we make ourselves actually improve reliability and serviceability. On that front, the answer is yes for the motion system and electronics, moderate for the enclosure, and intentionally minimal for commodity hardware. That balance keeps the machine repairable without pretending every bolt was forged in our own workshop.
Will the Design Adapt as Your Products Change?
A design that cannot flex when your product evolves will quickly feel outdated. Instead of treating the layout as a fixed arrangement, think of it as a set of rules that can be recombined. When you add a new product line or shift priorities, the interface should adapt by adjusting components rather than requiring a full redesign.
Modular thinking makes this possible. If every element depends on global styles and hard-coded dimensions, even a small change can cause a cascade of breakage. By working with reusable blocks and relative spacing, the team can test new structures without losing visual consistency.
A useful way to check whether your design is truly adaptable is to remove or swap one product module and see how the rest responds. If the layout holds up and stays easy to navigate, you are in good shape. If you find yourself rebuilding large sections, the design is still too rigid, and that rigidity will slow down every future product change.
Are Lead Times Backed by Real Production Data?
Lead times sound reassuring on paper, but the real question is whether those numbers reflect what's actually happening on the shop floor. Many companies quote standard lead times pulled from a spreadsheet that hasn't been updated in months, or worse, a guess someone made years ago. Without pulling live data from production scheduling, machine run rates, and material availability, a promised lead time is just a polite fiction.
When lead times are genuinely backed by real production data, you can see the logic: current backlog, actual cycle times, scrap rates, and labor capacity all feed into the estimate. That means the date you give a customer isn't a wish—it's a calculation. The difference shows up fast. One shop might say "three weeks" because that's what they've always said, while another says "18 days" because the system looked at the queue for that specific part number and the next open slot on the right machine.
If you can't trace a quoted lead time back to a live data point from the factory floor, treat it as a placeholder, not a promise. Real data-backed lead times shift when conditions shift—they get shorter when a line is underloaded, longer when a key material is delayed. Static lead times, on the other hand, stay the same until someone remembers to change them, which is usually too late.
Do They Have References From Lines Similar to Yours?
References only matter when they come from operations that actually resemble yours. A list of logos from unrelated industries won't tell you how a machine handles your specific film tension, fill volume, or sanitary requirements. Press for details about materials, line speeds, and changeover patterns instead of accepting a generic “we have many satisfied customers.” The closer the reference line is to your daily reality, the fewer surprises you will face after installation.
Ask for a walkthrough of a recent project that had similar constraints, such as tight temperature windows, abrasive ingredients, or short batch cycles. Then dig into the ugly parts: where did the line underperform at first, and what did the supplier change to fix it? If the vendor can name a specific adjustment made to a reference line’s infeed or vision system, that signals hands-on problem solving rather than sales polish. Generic praise without operational detail rarely predicts how your own startup will go.
A lack of exact-match references is not always a dealbreaker, but it shifts more risk onto you. In that case, ask for a paid trial on your product or a detailed engineering study before committing. If the supplier hesitates to run samples or connect you with a plant engineer from a similar line, take that as a warning. The best vendors treat reference conversations as a chance to show how they adapt their equipment to real production, not as a trophy wall.
FAQ
Look beyond glossy brochures and ask about their engineering team's hands-on experience with different extrusion setups. A partner worth considering will openly discuss screw design, roll stack configurations, and how they fine-tune melt temperatures for various resins. If they can walk you through past troubleshooting cases without hesitation, that's a strong signal of genuine know-how.
It's often the difference between a line that merely runs and one that fits your production reality. Standard machines rarely match every plant layout, polymer blend, or thickness target. A good builder will modify barrel lengths, adapt downstream units, or reconfigure control systems based on your specific output goals rather than forcing you into a generic package.
You need more than a phone number. Expect clear response-time commitments, remote diagnostics, readily available spare parts, and technicians who can guide your crew through recalibration or unexpected wear issues. The best partners treat your uptime as their responsibility months and years after installation, not just during the warranty window.
Request documented examples of lines running similar materials, whether that's PET, PP, PS, or multilayer structures. Ask about screw metallurgy, surface treatments, and temperature control ranges relevant to your resin's viscosity and sensitivity. A builder who has successfully processed challenging materials like high-impact or recycled blends will know the thermal and mechanical pitfalls to avoid.
Think about where your business will be in three to five years, not just next quarter. The right manufacturer can deliver a line sized for current demand while leaving room for higher throughput, additional downstream modules, or automation upgrades. Scalability means you won't have to replace the entire system when your sheet width or output requirements grow.
Look for traceability in their manufacturing process: documented inspections of critical components, alignment checks after assembly, and test runs with actual polymer before shipping. On-site acceptance testing is particularly valuable. If they encourage you to witness the line producing sheet to your specifications before it leaves their floor, that transparency usually reflects solid internal discipline.
Dig into energy consumption per kilogram of output, expected lifespan of screws and barrels, and how easily wear parts can be sourced or replaced. A slightly higher upfront price often pays off through reduced scrap rates, lower maintenance hours, and better resale value. Ask existing customers about unexpected costs they encountered during the first two years of operation.
Clarify whether the quoted lead time includes design approval, component sourcing, assembly, and commissioning. Delays often hide in sub-supplier bottlenecks or last-minute engineering changes. A reliable partner will provide a phased schedule with milestones you can verify, and they'll be upfront about any risks that could shift the installation date rather than promising an unrealistic turnaround.
Conclusion
Choosing a plastic sheet machine manufacturer involves far more than comparing specs on a brochure. You need a partner who will actually run your material through their equipment before you commit—seeing how your specific resins, fillers, or recycled content behave under real process conditions reveals issues that spec sheets hide. Once the machine is installed, after-sales support matters just as much as the sale itself: ask for clear response times, spare parts availability, and whether service engineers can dial in remotely or must fly out. Also dig into how much of the machine is built in-house. A company that makes its own screws, barrels, rolls, and control systems can iterate on quality much faster than one that assembles outsourced components, and that directly affects long-term uptime and precision.
The right manufacturing partner also proves their ability to adapt as your product lines shift. Whether you move to thinner gauge films, higher output, or new polymer blends, the machine's control architecture and downstream components should be flexible enough to handle those changes without a full rebuild. Ask for real production data behind quoted lead times—weekly build progress, testing schedules, and shipping milestones—not just optimistic estimates. Finally, insist on references from lines similar to yours. A supplier who has successfully commissioned machines for comparable sheet widths, thicknesses, and output rates will understand your operational pain points far better than one learning on your dime. These factors separate a vendor from a genuine long-term partner.
Contact Us
Contact Person: LISA LEE
Email: [email protected]
Tel/WhatsApp: +86 13780696467
Website: https://www.qdpipemachine.com