Reliable Cast Parts Which One Should You Choose
2026-09-30
Selecting cast parts that won't let you down is harder than it sounds. Too many suppliers promise durability, but few back it up when the pressure is on. If you're tired of second-guessing every component, it's time to look at what makes a casting truly reliable. At Zhaoyuqi, we've built our reputation on parts that perform—not just on paper, but in the real world.
The Hidden Trade-Offs Between Cast Iron, Steel, and Aluminum
Cast iron earns its reputation for heat retention, but that same density means it responds slowly to temperature changes. You might wait several minutes before the pan surface actually drops after lowering the burner, which can be frustrating when you need quick adjustments. Steel sits somewhere in the middle, heating more evenly than cast iron but still demanding patience if you're used to lighter cookware. Aluminum, by contrast, reacts almost instantly—yet that speed comes with its own compromise, as it cools down just as fast when food hits the surface.
Durability is another area where the trade-offs hide in plain sight. Cast iron can survive decades, even generations, but it demands regular seasoning and refuses to tolerate harsh detergents or long soaks. Steel offers a bit more forgiveness, though it still rusts if left wet and requires more oil than most home cooks expect. Aluminum is lightweight and resistant to corrosion in its natural state, but it's soft, easily scratched, and prone to warping under high heat unless you invest in a heavier anodized version.
Perhaps the least discussed factor is how each metal interacts with acidic foods. Tomato sauces, wine reductions, or lemon-heavy dishes can strip seasoning from cast iron and leave a metallic aftertaste. Steel is more stable but not immune, especially if the pan hasn't built up a solid patina. Aluminum reacts strongly with acids, which is why uncoated aluminum pots are rarely recommended for long simmers. None of these materials is universally perfect—each excels in one scenario while quietly compromising in another.
Sand Casting vs. Die Casting: Choose Wrong and You'll Pay for It
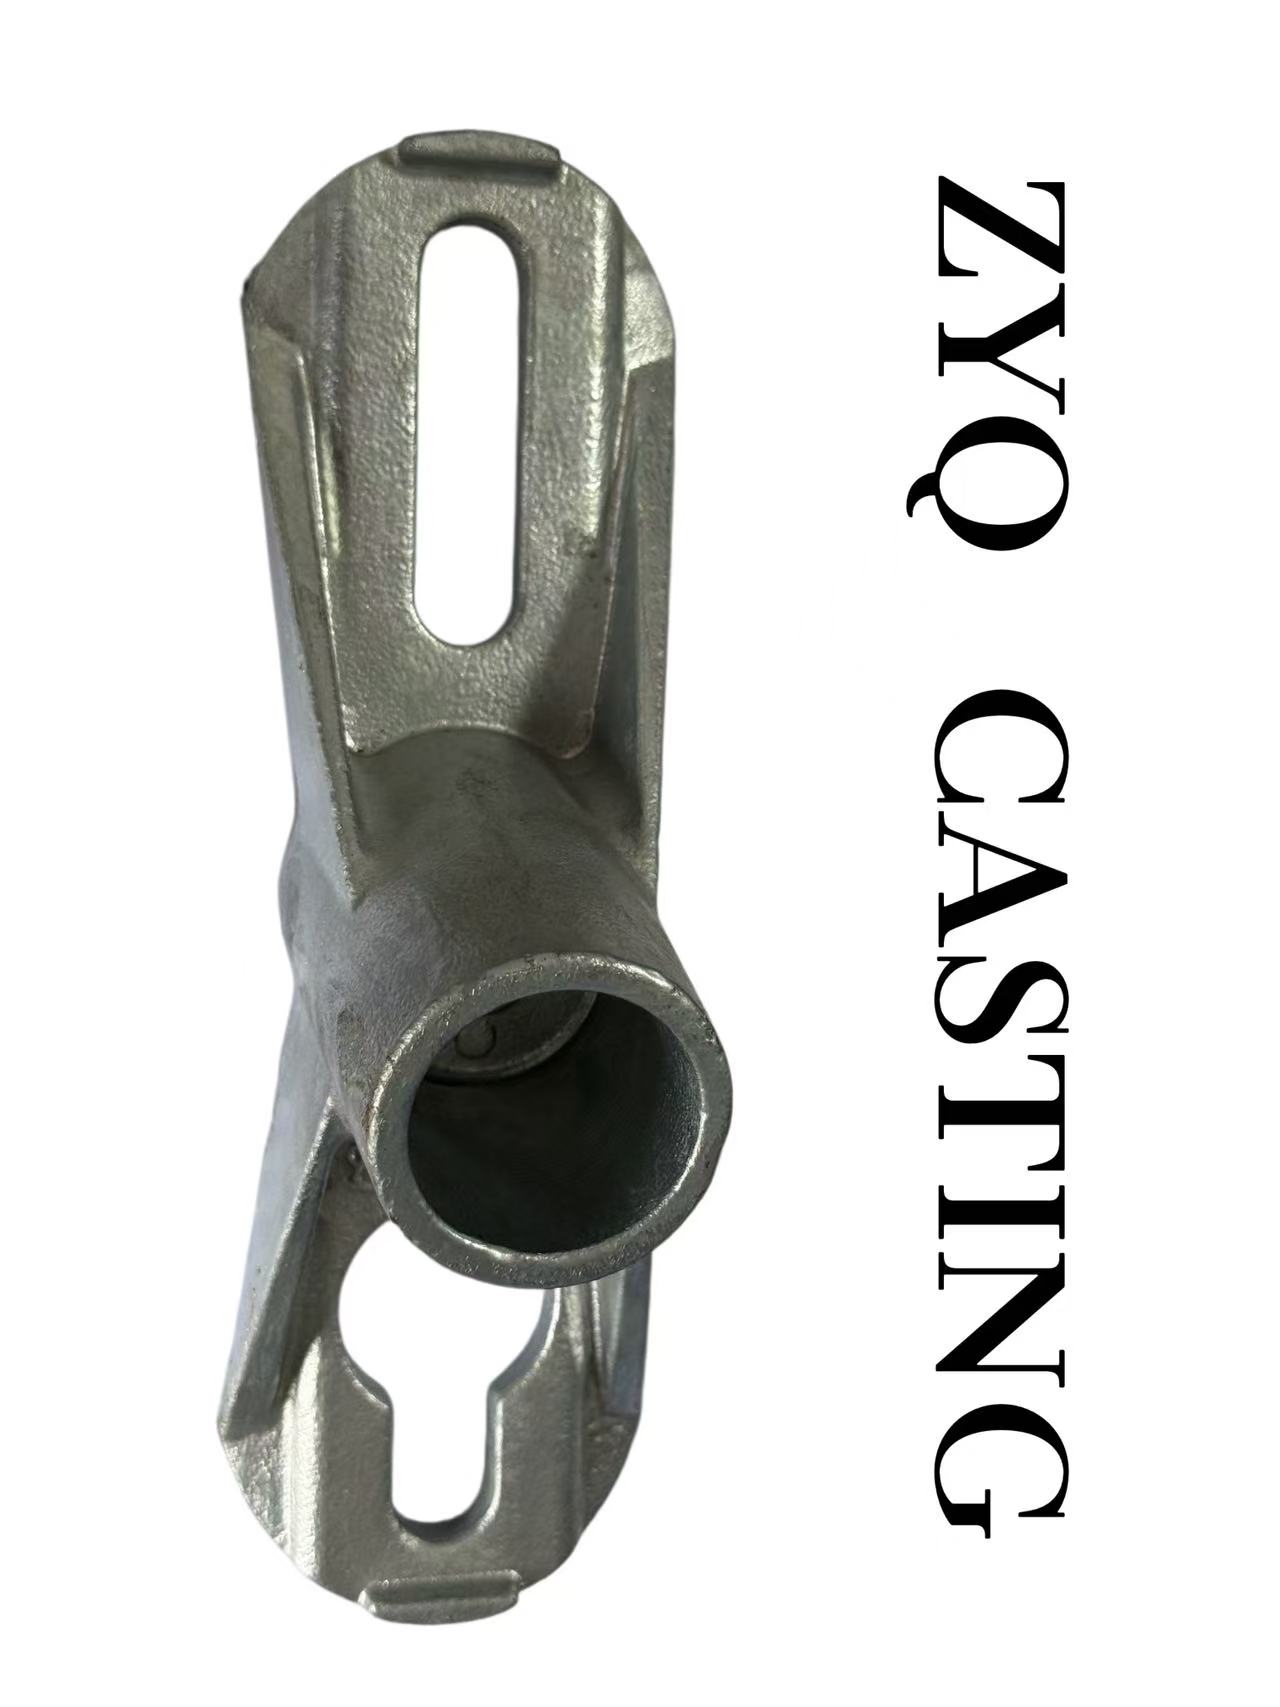
The choice between sand casting and die casting isn't a coin flip—it's a financial decision that many shops get wrong. Sand casting looks cheap because the tooling costs almost nothing, but if you're running thousands of parts, the per-unit labor and finishing will eat you alive. Die casting, on the other hand, demands a hefty upfront investment in steel molds, so using it for a handful of prototypes is like buying a race car to drive to the corner store.
The real trap is ignoring your alloy. Sand casting handles ferrous metals like iron and steel with ease, while die casting is mostly limited to zinc, aluminum, and magnesium. Try to die cast stainless steel and you'll destroy the mold in a shift. Also, wall thickness matters: die casting shines with thin, intricate walls and tight tolerances, but sand casting struggles below 5 mm and leaves a rough surface that needs extra machining. If you need a smooth, near-net-shape part, sand casting will force you into secondary operations that blow your budget.
Here's a rule that saves money: for under 500 pieces, sand casting usually wins despite the slower pace. For over 5,000 pieces, die casting's speed and consistency pay for the mold many times over. Between those numbers, you need to calculate scrap rates, heat treatment, and assembly costs—not just piece price. Choose wrong, and you'll either pay for a die you never fully amortize or drown in grinding and rework from sand castings that should have been die cast from day one.
Why 'Standard' Tolerances Are a Recipe for Assembly Problems
The phrase "standard tolerance" sounds reassuring until you realize it's often a shorthand for "whatever the machine shop defaults to." In assembly, those defaults rarely account for how multiple parts interact. A ±0.005 inch on a single bracket might seem generous, but stack three or four such parts together and you're suddenly looking at a combined variation that eats up your entire design clearance. That's when bolts refuse to line up, dowel pins jam, and mating surfaces leave ugly gaps nobody planned for.
Another hidden trap is that standard tolerances ignore the direction of error that actually matters. A hole can be oversized or a shaft undersized and still assemble, but the reverse creates interference. Generic callouts don't distinguish between these conditions. They simply spread the allowed deviation symmetrically, often on both sides of nominal, which is statistically convenient but mechanically naive. The result is a stack of parts that each pass inspection yet fail to fit together on the line.
The real cost shows up during final assembly, not in CAD. Operators start hand-filing brackets, force-fitting connectors, or loosening torque specs just to get things seated. Every ad hoc fix adds labor time, scrap risk, and warranty exposure. The alternative isn't obsessive precision everywhere; it's assigning tolerances based on the actual function and the accumulated variation across the whole assembly. Leaving that to a blanket standard is how small mismatches become expensive habits.
The One Supplier Question That Reveals Everything About Quality
Ask any sourcing manager what they look for in a supplier and you'll hear about tolerances, certifications, and turnaround times. But the question that actually cuts through the noise is simpler: "What do you do when something goes wrong?" It sounds almost too basic, yet the answer exposes more about a supplier's true quality culture than a stack of inspection reports ever could. A supplier that hesitates, blames the customer, or claims defects never happen isn't just being modest—they're revealing that they lack a healthy process for failure.
The best suppliers don't wait for you to discover a rejected batch. They have a structured way to flag issues early, run root cause analysis, and share corrective actions without being asked twice. When you ask that question, watch their body language and listen for specifics. Do they mention containment plans, communication timelines, or traceability? If they give you a concrete, unscripted answer, you're likely dealing with a partner who treats quality as an ongoing discipline rather than a final inspection checkbox.
Lead Time Myths: When a Longer Wait Means a Better Cast Part
There's a stubborn belief in procurement circles that a shorter lead time signals a more capable foundry. But cast parts don't behave like off-the-shelf hardware. Rushing a pour often means skipping the very steps that keep porosity, shrinkage, and residual stress in check. A longer wait can be the difference between a casting that holds a tolerance and one that needs rework after machining.
The real bottleneck isn't always capacity—it's metallurgical patience. Certain alloys need slower cooling in the mold to develop the right grain structure. Post-cast heat treatment, stress relief, and inspection aren't optional add-ons; they're where reliability is earned. When a foundry compresses that timeline, they're not saving time, they're shifting cost and risk downstream to your assembly line.
None of this means every long lead time is justified. A disorganized shop can be slow for all the wrong reasons. But if the extra weeks come with documented process controls, controlled shakeout temperatures, and rigorous non-destructive testing, the wait may be buying you a part that won't fail in the field.
From Prototype to 10,000 Units: Scaling Without Losing Integrity
Moving from a hand-built prototype to a production run of ten thousand units is rarely a linear journey. The early versions are often refined through personal attention, quick fixes, and materials that simply won't survive high-volume manufacturing. The real challenge begins when you try to preserve the feel, fit, and finish that made the original piece special while introducing jigs, injection molds, or automated assembly lines. Many small studios underestimate how much of the prototype's character lives in the tiny imperfections—the slight radius on an edge, the particular tension of a spring, the way two surfaces meet. Replicating those details at scale requires more than just a technical drawing; it demands a clear definition of what must remain untouched and what can evolve without breaking the product's identity.
A practical approach is to treat the scaling process as a series of controlled experiments rather than a single leap. Start with a pilot batch of a few hundred units, built using the same tools and materials intended for full production. Measure everything that matters: dimensional tolerances, surface texture, assembly time, and even the sound a latch makes when it closes. Compare each pilot unit against the original prototype not just with calipers, but with the same hands and eyes that approved the first one. Document the differences, then decide which are acceptable trade-offs and which are deal-breakers. For example, a slight change in the grain of a molded plastic part may be invisible to most customers, but a looser hinge or a sharper corner could destroy the perceived quality. By isolating these variables, you can adjust tooling, refine processes, and retrain assemblers before committing to the full run.
Integrity at 10,000 units is not about freezing the prototype in time; it's about translating its intent into a repeatable system. That means writing down the tacit knowledge that was once in the maker's head—acceptable ranges for every dimension, the order of operations for each subassembly, even the environmental conditions in the workshop. It also means building relationships with suppliers who understand that consistency is a feature, not a limitation. Some manufacturers achieve this by keeping one original prototype on the production floor as a reference standard. Others create a simple go/no-go test that any line worker can perform in seconds. The goal is to make the right thing easy to do and the wrong thing hard to do accidentally. When scaling succeeds, the ten-thousandth unit should feel as deliberate as the first, even if it was produced in minutes rather than days.
FAQ
Start with the material's mechanical properties and the casting method's typical soundness. Ask for tensile test data and X-ray or ultrasonic inspection results, not just dimensional checks. Porosity and inclusions matter far more than surface finish in high-stress parts.
No, that is a common misunderstanding. Sand casting handles large parts and can be extremely reliable when the foundry controls sand quality, pouring temperature, and cooling rates. Investment casting excels at small, intricate parts with better as-cast surface finish. Reliability has more to do with process discipline than the method name.
Look beyond their brochure. Request a trial run of a small batch and measure variation across parts. Check if they track scrap rates, use statistical process control, and keep records of chemical analysis for each heat. A foundry that shares its reject data openly is usually more trustworthy than one that only shows polished samples.
Duplex stainless steel or nickel-aluminum bronze are strong choices because they resist pitting and crevice corrosion without needing heavy coatings. Cast iron will rust quickly unless you add a barrier coating, but that coating becomes a maintenance burden. Match the alloy to the specific salinity and temperature rather than assuming all stainless grades work.
Sometimes, if the part is non-structural and easy to replace. But in load-bearing or safety-critical components, a low upfront price often hides higher rejection rates, hidden porosity, or inconsistent dimensions. You may end up spending more on sorting, rework, and field failures than you saved on the purchase order.
Shrinkage cavities, gas porosity, cold shuts, and sand inclusions are the usual suspects. Most of these sit below the surface, so do not rely on visual inspection alone. Cut a few samples from each batch, or ask for radiography on critical sections. If a supplier refuses to allow sectioning, treat that as a red flag.
Correct heat treatment relieves internal stresses, refines grain structure, and can boost toughness or hardness. Skipping it or using the wrong cycle can leave residual stress that causes warping or cracking later, especially after machining. Always confirm the foundry follows the exact cycle for your alloy and provides furnace charts with each batch.
You can, but do not simply copy the forged design. Castings allow more complex shapes, but they also need generous radii, uniform wall thickness, and well-placed risers to avoid weak spots. Work with the foundry during design to place parting lines and gates away from high-stress areas. A direct material-for-material swap without redesign often fails.
Conclusion
Choosing a reliable cast part rarely comes down to a single material or process. Cast iron, steel, and aluminum each carry hidden trade-offs that only surface under real operating loads. A component that looks identical on a drawing may crack, warp, or wear differently depending on the alloy's thermal history and internal grain structure. The same logic applies to casting methods. Sand casting offers flexibility for low volumes and complex geometries, but its dimensional scatter can haunt assembly later. Die casting delivers speed and repeatability, yet forces you into design constraints that may weaken the part. What often gets overlooked is the tolerance spec. Accepting a 'standard' tolerance because it is common invites fit problems. A truly reliable supplier will push back and ask how the part actually mates with its neighbors, then adjust the process to hold the real critical dimensions.
Quality becomes visible only when you ask the one question most buyers skip: "How do you validate your process when I'm not watching?" The answer reveals whether the foundry relies on inspection after the fact or builds control into the pour, the cooling, and the finishing. Lead times are another trap. A shorter wait often means corners were cut in heat treatment or stress relief. A longer wait can be a sign of proper aging, testing, and documentation. Scaling from a single prototype to 10,000 units tests a supplier's discipline more than their equipment. The parts that survive volume production are those whose original design respected the casting process, not fought it. Choosing a reliable cast part therefore means choosing a supplier who understands material behavior, tolerance reality, and process stability before any metal is poured.
Contact Us
Contact Person: Nico Yin
Email: [email protected]
Tel/WhatsApp: 8618561567088
Website: https://www.ductileironparts.com/