Top Solar Ground Mounting System Factories in China Worth Knowing
2026-08-23
China has quietly become the backbone of the global solar supply chain, and ground mounting systems are no exception. While most buyers focus on panels and inverters, the factories behind the steel and aluminum structures often decide whether a project stays on schedule—or goes over budget. In this list, we skip the generic names and highlight the ones with real engineering depth, consistent export quality, and the flexibility to handle custom terrain. One name that keeps coming up in recent bids is Egret Solar, a player that has moved beyond copy-paste designs to offer wind-tunnel-tested racking for harsh sites. If you are sourcing for utility-scale or commercial projects, the following factories deserve a closer look before you sign your next PO.
Factories That Turn Harsh Terrain into Energy Hubs
A windswept plateau in Patagonia, a sun-scorched stretch of the Atacama, a fjord carved by ancient ice—these are not backdrops for survival documentaries but the front lines of a quiet industrial shift. Here, factories designed for extraction have given way to plants that harvest the elements. Instead of fighting the land, they anchor themselves to it, turning relentless gusts, blinding sunlight, and river-fed gradients into steady streams of power. The buildings themselves look almost temporary: low-profile structures with turbine halls sunk into rock, solar arrays that follow the sun like mechanical sunflowers, and pipelines that disappear into mountain shadows.
What makes these sites compelling is not raw output but fit. A geothermal plant in Iceland sits nearly invisible against a lava field, its only trace a faint plume of steam that could pass for a hot spring. In the Gobi Desert, a combined solar and wind facility uses the very dust that buries roads to cool its inverters, while its transformers are raised on stilts to let sand blow through. Engineers on the ground talk less about efficiency curves and more about reading the land—where the wind bends, how the snow drifts, when the river swells. One project manager described the process as “teaching a factory to breathe with the terrain instead of against it.”
These energy hubs also reshape local logic. A plant built on a former mining site in the Andes now shares its access roads with herders, and its control room doubles as a weather station for nearby villages. The harshness that once made such places marginal—altitude, aridity, isolation—becomes the reason they work. There is no need to displace anyone, no farmland lost, no forest cleared. Just machines and people finding a rhythm in places most maps still mark as empty.
Inside the Welding Lines Where Corrosion Resistance Begins
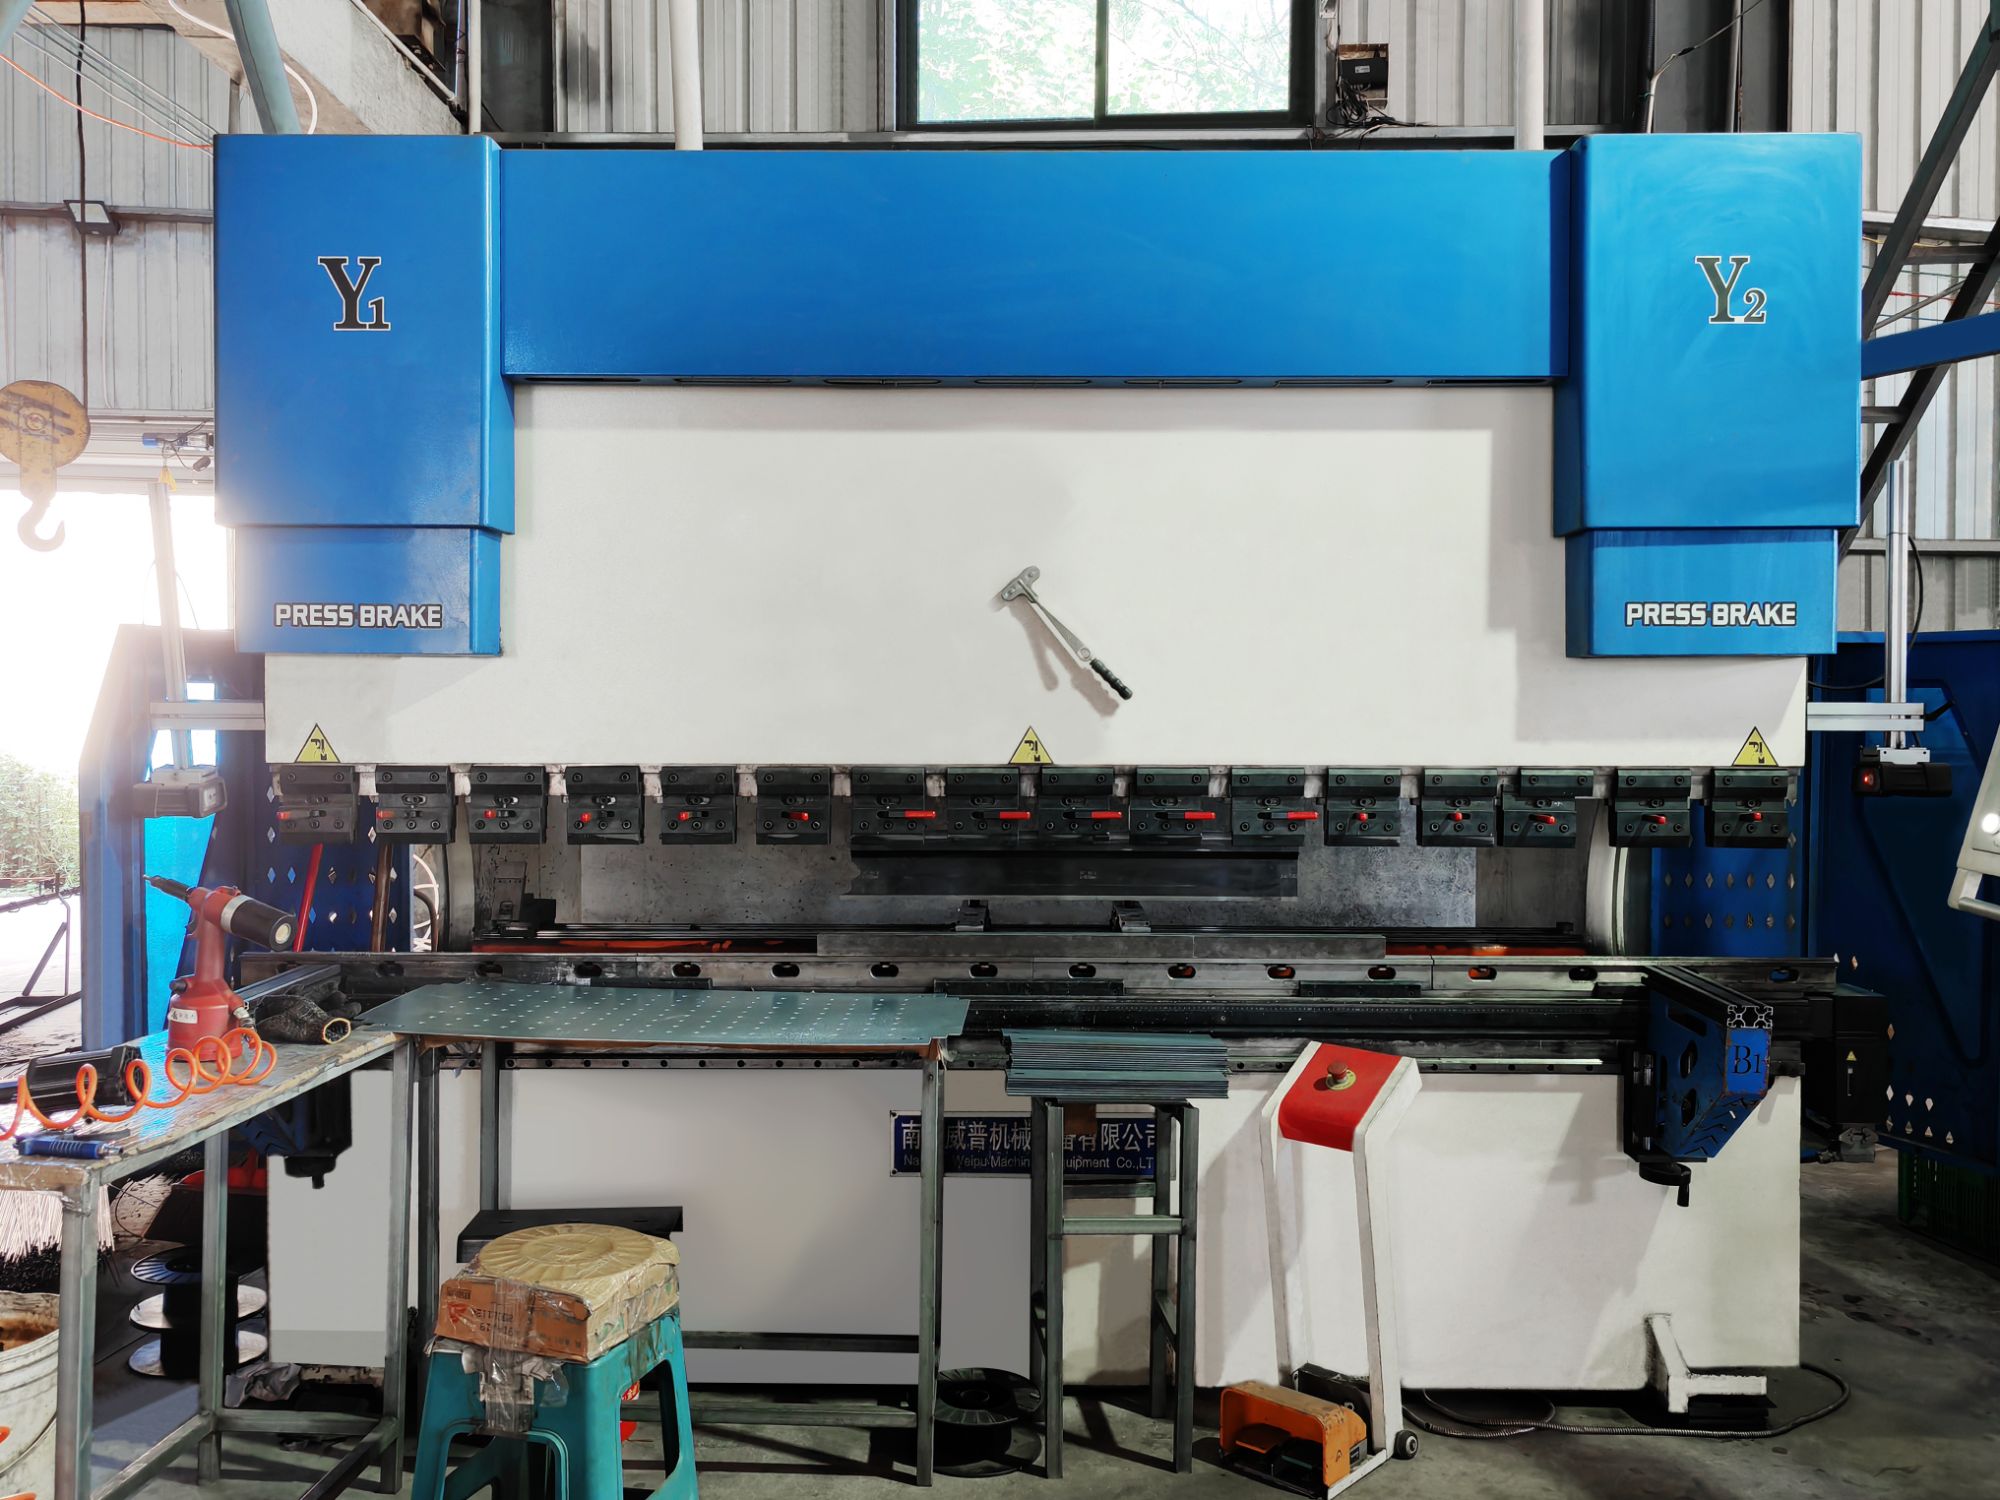
The weld zone is often where a material's true corrosion resistance is either forged or lost. Here, at the intersection of heat, filler metal, and base alloy, the microstructure shifts in ways that can invite attack from moisture, chlorides, or process chemicals. A bead laid too hot may leave chromium carbides decorating the grain boundaries, quietly stripping the nearby steel of its protective oxide layer. Conversely, a carefully controlled heat input and the right filler chemistry can preserve the alloy's passive film right through the fused region, making the joint as noble as the parent metal.
Experienced fabricators know that corrosion rarely starts on a flat, untouched surface. It begins in the tiny crevices, the undercut toes, the spatter dots, and the heat-tinted bands that frame every weld. These discontinuities trap water, concentrate chlorides, and create oxygen-depleted cells where pitting can initiate. That's why the most corrosion-resistant welds aren't just strong—they are smooth, fully fused, and free of sharp transitions. A slight change in travel speed, shielding gas flow, or interpass temperature can mean the difference between a joint that lasts decades and one that starts rusting before the scaffolding comes down.
In stainless and duplex alloys, corrosion resistance is not a surface coating but a bulk property—and the weld must preserve it from root to cap. Post-weld cleaning, pickling, and passivation restore the chromium oxide layer that welding inevitably disrupts. Yet the first line of defense is engineering the weld itself: matching filler metal composition, minimizing dilution, and controlling ferrite content in austenitic welds. When those parameters align, the weld line stops being a weak link and becomes a seamless continuation of the alloy's inherent resistance—a place where corrosion simply has no foothold.
How Custom Racking Designs Cut Installation Time in Half
Most warehouse managers expect racking installation to drag on for days, with crews re-drilling holes and shimming beams to force standard components into spaces that never quite fit. Custom designs flip that dynamic. When uprights, beams, and decking are fabricated to the exact bay widths and ceiling heights of a specific building, the on-site work becomes mostly bolt-together assembly. There is no guesswork about where a crossbeam should sit or whether a frame will clear a sprinkler line. The drawings already accounted for those obstacles, so installers spend their time tightening connections instead of solving layout puzzles.
Another time sink that custom racking eliminates is field modification. Off-the-shelf systems often arrive with long lead times and still require cutting posts or re-spacing shelves to accommodate odd pallet sizes or uneven floors. With a custom approach, those adjustments happen in the engineering phase, not on the warehouse floor. Components arrive pre-punched, pre-cut, and sometimes even pre-assembled into larger modules. A crew can set an entire run of racking in a morning because every piece has a predetermined place. There is no need to stop and call the office for approval on a workaround.
The reduction in installation hours also comes from fewer trades on site at the same time. When racking fits the first time, electricians and sprinkler contractors do not have to wait for adjustments before completing their own work. This overlap, or lack of it, keeps the project schedule tight. In practice, facilities that switch to custom designs often report cutting the racking phase from two weeks to three or four days. That is not a minor improvement; it means the warehouse can start receiving inventory while competitors are still sweeping up metal shavings.
The Certification Trail: Why UL and TÜV Matter More Than Ever
The UL and TÜV marks have long stood for safety, but their role now extends far beyond a simple compliance check. As electronics become more interconnected and complex, the stakes of failure are higher. These certifications offer a shared language that helps manufacturers, regulators, and consumers build trust in a crowded marketplace where claims are cheap and proof is scarce.
Not so long ago, certification might have been treated as a hurdle to clear before launch. Today, with supply chains fragmented across regions and components sourced from multiple vendors, a single weak link can undermine an entire product line. UL and TÜV's rigorous testing protocols don't just validate the final product—they scrutinize production processes and materials, turning certification into a tool for risk management rather than paperwork.
What's more, as sustainability and energy efficiency become central to purchasing decisions, these bodies have evolved their standards to include lifecycle assessments and performance claims. For brands, earning certification is no longer a "nice to have"—it's a way to demonstrate integrity and long-term reliability in an environment where scrutiny is intense and trust is hard-won.
From Port to Project Site: Logistics That Keep Deadlines Alive
Every hour a container sits at the dock, the schedule slips a little further out of reach. We treat port congestion not as an abstract risk, but as a physical obstacle to be mapped and moved around. Our teams track vessel ETAs against real-time terminal throughput, pre-clearing customs paperwork before the ship even ties up. That means the moment a crane lifts your cargo off the deck, it’s already moving toward the project site—not waiting in a queue of trucks that showed up too late.
The real test comes in the last fifty miles. A single missed turn or an unannounced road closure can undo weeks of careful planning. So we don’t just dispatch a driver; we build a route narrative. Each delivery is scouted ahead of time—bridge heights measured, weight limits confirmed, alternate paths marked for after-dark permits. When the unexpected happens, the driver isn’t improvising alone. A dedicated coordinator reroutes in real time, keeping the site team informed before the delay becomes a problem.
Deadlines aren’t protected by luck. They’re protected by the boring, unglamorous work of checking and rechecking every link in the chain. From port agent handshakes to the final crane lift at the laydown yard, we document each transfer, photograph every load, and log the exact minute it arrives. That record isn’t just for billing—it’s proof that when we promised a delivery window, we meant it. And when the next shipment comes through, we already know exactly where the last one lost an hour.
When a 50-Megawatt Order Tests a Factory’s True Capacity
A 50-megawatt order doesn’t just fill the schedule—it strips away any slack. The rated capacity on paper assumes clean material flows, zero downtime, and a workforce running at full clip. Within the first week, the real constraints surface: a solder station that trips every forty minutes, a lamination cycle that runs six seconds longer than the OEM spec, and a warehouse aisle that can’t stage more than nine pallets of glass at once.
Shift supervisors start tracking minutes, not just units. They discover that the line loses 11% of its theoretical output to changeovers and minor stops. Instead of adding a second shift, the plant reroutes bypass conveyors and resets the stringer spacing to cut scrap from 2.3% to 1.7%. A quality gate that used to sample every 200 panels now samples every 80, and that alone saves a half-day of rework by catching micro-cracks earlier.
Suppliers feel the pressure too. The usual three-day buffer on junction boxes evaporates, forcing the buyer to split shipments between two regional distributors. One batch arrives with connector pins bent at a 3-degree angle—acceptable by spec, but enough to slow the insertion jig. The factory’s true capacity ends up being not the nameplate 1.8 megawatts per day, but 1.5 megawatts sustained over three weeks. And that number only holds if the air compressor keeps up.
FAQ
Arctech Solar, Antaisolar, and Grace Solar frequently handle large utility projects, offering both tracking and fixed-tilt systems with in-house galvanizing or coating lines.
Arctech is known for its multi-point drive tracking systems and has supplied gigawatt-scale plants in harsh environments, including deserts and high-wind zones.
Look for wind tunnel test reports, finite element analysis, and certifications like UL 3703 or IEC 62817. A factory with its own test lab usually gives more dependable data.
Firms like Mibet and Clenergy often supply pre-assembled kits, layout drawings, and remote installation guidance, which helps reduce field errors.
Jiangsu Guoqiang and Shanghai Ensure Machinery use hot-dip galvanizing and magnesium-aluminum-zinc coatings to extend life in salty or wet conditions.
Pricing varies with steel thickness, coating type, and tracker complexity. Generally, fixed-tilt systems from large integrated mills cost less than tracker systems from R&D-heavy suppliers.
Most top factories quote 15 to 30 days after design freeze, but large utility orders or special coatings can stretch to 45 days or more.
Many export full systems—posts, rails, clamps, fasteners, and even torque tubes—packed in containers with clear assembly markings.
Conclusion
China's leading solar ground mounting system manufacturers have moved far beyond basic racking production. Teams that once saw rocky slopes or flood-prone land as deal-breakers now treat them as opportunities, reshaping uneven terrain into stable energy hubs with reinforced foundations and adjustable leg designs. On the factory floor, the welding lines tell the same story of resilience—automated seam tracking and zinc-aluminum coating baths give steel frames the corrosion resistance needed for coastal deserts and humid river valleys. Custom racking layouts, pre-assembled in labelled bundles, cut on-site installation time by as much as half, allowing EPC crews to bolt modules into place without field drilling or cutting.
Behind that speed sits a certification trail that has become non-negotiable. UL 3703 and TÜV Rheinland listings now decide which Chinese factories get shortlisted for utility-scale tenders, and the best plants keep test reports updated for every batch. From port to project site, these manufacturers run their own container loading plans and inland barge routes, so a delayed vessel does not automatically stall a 50-megawatt installation. When such a large order lands, capacity is tested not just by welding speed but by how quickly jigs are swapped, how many containers leave per week, and whether the factory can hold dimensional tolerances across thousands of identical posts. The factories worth knowing are the ones that treat all six of these links as one continuous chain.
Contact Us
Contact Person: Leite
Email: [email protected]
Tel/WhatsApp: (+86)13666072898
Website: https://www.egretsolars.com/